Case Study: Automated Floor-Level Package Conveying in the Food Industry
Optimizing Material Handling Flows with an Automated Conveying Solution
In the food processing industry, optimizing logistics flows is a key factor in improving productivity, reducing the physical strain of workstations, and ensuring the safety of material handling operations. We recently partnered with a poultry producer to fully automate its floor-level parcel conveying and storage systems.
Strenuous Manual Handling
Avant l’installation de notre solution de convoyage, les opérateurs réalisaient l’ensemble des manipulations nécessaires à la production de viande manuellement.
Après les opérations de pesée et d’étiquetage, chaque colis était soulevé puis déposé sur une palette. Une fois celle-ci remplie, elle était déplacée vers une zone de stockage située dans une pièce voisine.
Cette organisation présentait plusieurs limites :
- une forte sollicitation physique des opérateurs ;
- un risque élevé d’apparition de troubles musculo-squelettiques (TMS) ;
- une cadence de production limitée par la perte de temps liée à la manutention manuelle des colis de viande.
A floor conveyor solution tailored to the demands of the food processing industry
To address these challenges, OCA designed and installed fully automated floor conveyors to streamline the transport of packages throughout the production process.
Two modular mesh conveyors were installed along the workstations to serve all operators.
With this configuration, packages of various sizes (cartons and bins) are simply placed on the conveyors, virtually eliminating all manual operations. Operators need only push the packages onto the conveyor, with no manual handling required.
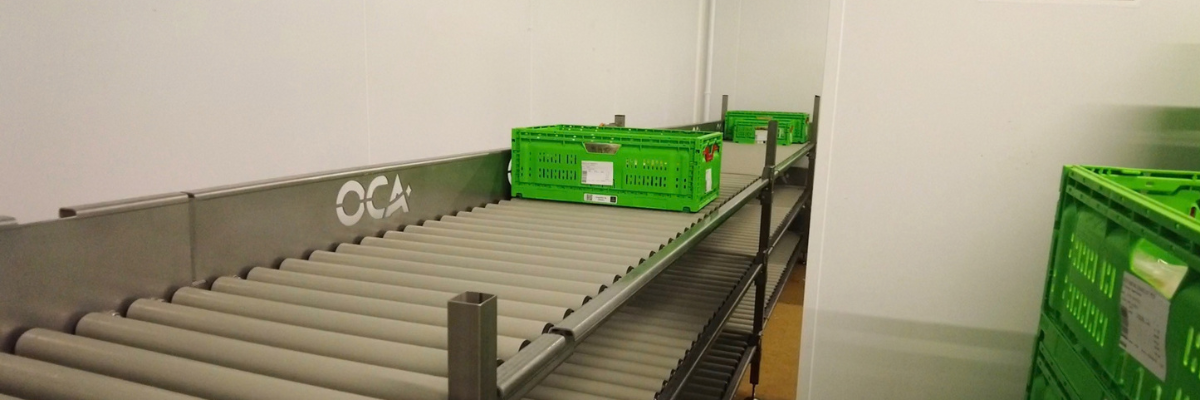
Up to 100 packages per hour are then automatically transported to a gravity storage area via a roller conveyor.
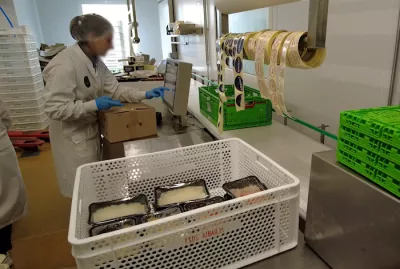
Modular mesh floor conveyor near workstations

OCA Floor Conveyor Detection Sensors

Swivel conveyor serving the three storage levels